
Dispersion strengthening
What is dispersion strengthening?
Dispersion strengthening is a metallurgical process that enhances the strength of a metal by introducing small, stable, particles of a different material (known as dispersoids) into its matrix. These particles act as obstacles to the movement of dislocations, which are defects in the crystal structure of the metal that allow it to deform. By inhibiting dislocation motion, the material becomes harder and stronger.
Key aspects of dispersion strengthening are:
- Dispersoid Particles: These are typically oxides, carbides, or other compounds that do not dissolve in the metal matrix at high temperatures. They are stable and remain finely dispersed throughout the material.
- Mechanism: Dislocations move through a metal when it is deformed. The dispersoid particles hinder this movement by pinning the dislocations or forcing them to bypass the particles, a process known as Orowan bowing. This increases the strength of the metal.
- Thermal Stability: Unlike other strengthening methods (such as precipitation hardening), dispersion strengthening is more effective at elevated temperatures because the dispersoid particles are thermodynamically stable and resist coarsening.
- Applications: Materials that undergo dispersion strengthening are often used in high-temperature applications, such as turbine blades, nuclear reactors, or aerospace components, where strength at high temperatures is crucial.
How is it done?
The insoluble, second phase particles are introduced to the base metal.
In high strength engineering materials, second phase materials are the most potent strengthening agent. Common examples include are added to Iron-base, aluminium, nickel, titanium alloys.

The mechanical properties of an alloy are determined by the size, shape and number of second phase particles added
The effect of adding second phase particles dispersed throughout the matrix is to block dislocation motion, which then strengthens the material. In order for plastic deformation to occur, a much greater stress is now needed.
Orowan Mechanism
The disruption caused by dislocation can be seen in the Orowan (or dislocation bowing) mechanism diagram below.

- As a dislocation line approaches particles, a dislocation loop is formed around these particles, this process is called bowing.
- The dislocation loop formed then interacts with future dislocation lines.
- The movement of the dislocation is slowed down
- This slowing down increases the strength of the material.
The particle size and volume of alloying particles are key factors for determining the increased strength,
- Larger particles: the strengthening effect decreases
- Small particles: the strengthening effect increases
- Higher the volume of particles increases the strength as they will be tightly packed.
Oxide dispersion strengthened alloys (ODS alloys)
Adding other metals to a base metal is not the only way to change its properties. In this section we will focus on the addition of Oxides.
Oxide dispersion alloys are used where extreme operating conditions are expected, as they are highly resistant to creep and maintain good strength at high temperatures.
Applications include; high temperature turbine blades (thermal power stations), heat exchanger tubing, aerospace and within the nuclear industry.
The properties of ODS alloys greatly depend on the microstructure, such as the grain size of the alloy matrix, the morphology, size and distribution of the oxide second phase particles.
Most ODS alloys are prepared by sintering as shown below.
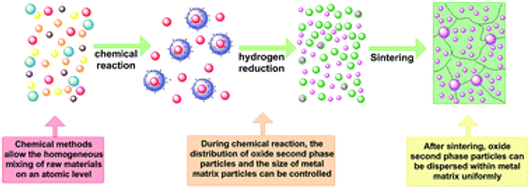
The primary factor for determining the microstructure and properties is determined by the composite powder precursor.
Oxide dispersion strengthened (ODS) alloys are produced by the mechanical alloying of powders.
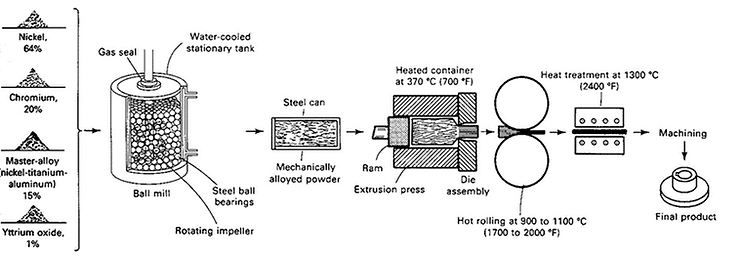
Figure 1 – ODS alloying process
The powder constituents can be in the elemental, intermetallic or pre-alloyed state.
- The metal and oxide powders are blended and mechanically alloyed using a ball mill, which is a grinder filled with steel balls placed in a rubber container, as the container rotates, the balls drop and impact with the powder, this reduces particle size.
- The powders become smeared together due to the repeated impacts.
- Shearing generates a fine mixture of the constituents.
- This powder is then packed into sealed containers, which are hot worked into simple shapes.
- The resultant product is dense and fine grained (less than 11µm) but has highly developed, directional residual strain.
- The alloys are then re-crystallised at about 1280-1350°C which forms large and highly elongated grains.
Case study
The effect of Al2O3 dispersion on the mechanical properties of Titanium Aluminide (TiAl).
The following section will compare the mechanical properties of a pure alloy of Titanium Aluminide with the alloy strengthened with Al2O3 dispersion.
The combination of mechanical properties for this alloy, at high temperatures, are superior to those of other superalloys.
Because of their high temperature specific strength and elastic modulus, low density along with good resistance against oxidation and corrosion, applications include low pressure gas turbine engines and various automotive applications
In this investigation 3% volume of Al2O3 is added to the alloy and test specimens were produced consisting of the TiAl alloy and the dispersion strengthened alloy, both samples have the same geometries.
Flexural bending testing was carried out across a high range of temperatures.

Stress strain curves were generated from the experimental data.
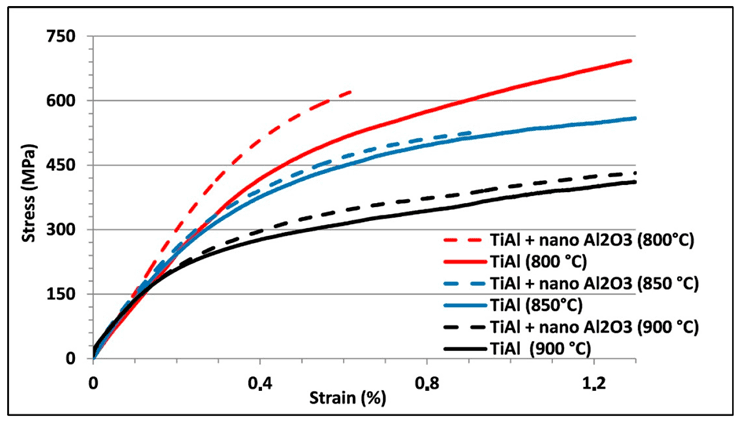
Figure 2 – Stress vs. strain curve from bending tests at various temperatures
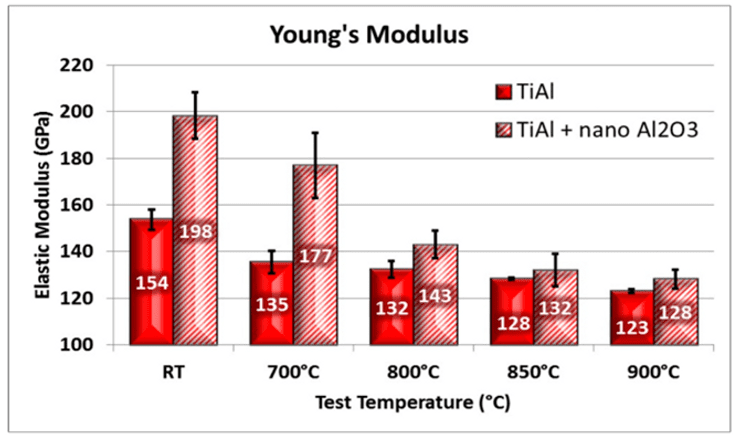
Figure 3 – Young’s modulus from bending tests at various temperature
Analysis
- As the temperature increases there is a general reduction in tensile strength.
- The young’s modulus decreases as temperature increases.
The trends are the same for both sample materials.
The dispersion strengthened alloy has a higher tensile strength at all operating temperatures.
The Young’s modulus is also higher at every temperature and corresponds to a maximum of a 30% increase at room temperature. The effect on Young’s modulus becomes significantly less at higher temperatures.
Conclusion
The results show dispersion strengthening is particularly effective in increasing strength at high temperatures, where other strengthening mechanisms lose their effectiveness.
Online Engineering Courses and Diplomas
To learn more about this topic or others in engineering, enrol on to one of our accredited online engineering courses today.
Why not check out the online engineering short courses specifically in manufacturing engineering:
Recent Posts
Laminar vs Turbulent Boundary Layers: Why Airflow Separates from Aircraft Wings
Laminar vs Turbulent Boundary Layers: Why Airflow Separates from Aircraft Wings Airflow around an aircraft wing is often shown as smooth streamlines passing neatly over the aerofoil. In reality, the thin layer of air immediately next to the wing surface behaves very differently from the undisturbed airflow further away. This region is called the boundary […]
Why There Is No Perfect Aerofoil: The Design Trade-Offs Behind Every Aircraft Wing
Why There Is No Perfect Aerofoil: The Design Trade-Offs Behind Every Aircraft Wing If a designer could create a perfect aerofoil, it would produce very high lift with almost no drag, remain stable at every angle of attack, fit a lightweight structure inside the wing and work equally well at low and high speed. No […]
How Aerofoils Generate Lift: A Beginner’s Guide to Angle of Attack, Camber and Pressure Distribution
How Aerofoils Generate Lift: A Beginner’s Guide to Angle of Attack, Camber and Pressure Distribution An aerofoil does not create lift simply because its upper surface is curved. Lift is produced because the aerofoil meets the airflow at a suitable angle and shape, causing a pressure distribution that results in an aerodynamic force. For aircraft […]